| Brands | Bohler |
|---|---|
| Product Types | Steels And Steel Alloys |
| Welding Process | MIG/MAG |
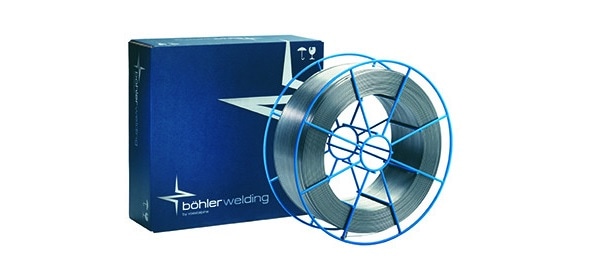
BOHLER DCMS-IG
AWS A5.28 / SFA-5.28 ER80S-G (ER80S-B2(mod.))
EN ISO 21952-A W CrMo1Si
TIG rod / wire, creep resistant
TIG rod and wire of type W CrMo1Si / ER80S-G for manual and mechanized gas tungsten arc welding. Compared to straight AWS B2 type filler metal, it offers an increased Manganese content supporting deoxidation behavior, reducing porosity, and improving strength after PWHT. The 1.25Cr-0.5Mo type weld metal exhibits a bainitic microstructure with favorable mechanical properties in tempered and quenched and tempered conditions. Under certain conditions applications in the as-welded condition is possible. The range of applications
covers joint welding of similar alloyed creep-resistant steel and steel casting. Approved for application under creep conditions at design temperatures up to 570 ºC. Due to the low content of residual and tramp elements, the weld metal offers a Bruscato factor < 12 ppm. Thus, being resistant to temper embrittlement and complies with the requirements on step-cooling testing.
TECHNICAL INFO:
Available in diameter’s : 1.2mm, 1.6mm
Yield strength : 440 MPa
Tensile strength : 570 MPa
Elongation : 23%
Related Products
-

 Welding Consumables
FOXcore 309L-T1
EN ISO 17633-A T 23 12 L P M21 (C1) 1
EN ISO 17633-B TS 309L-F M21 (C1) 1
AWS A5.22 / SFA-5.22 E309LT1-4(1) -
Welding Consumables
ECOspark 420
EN ISO 14341-A G 42 4 M21 3Si1 / G 42 4 C1 3Si1
AWS A5.18 / SFA-5.18 ER70S-6 -
Welding Consumables
FOXcore 316L-T1
EN ISO 17633-A T 19 12 3 L P M21 (C1) 1
EN ISO 17633-B TS 316L-F M21 (C1) 0
AWS A5.22 / SFA-5.22 E316LT1-4(1) -

 Welding Consumables
700